Material group · ASME B16.5 / EN 1092-1
Carbon Steel Flanges & Forgings — A105, A350 LF2, A694
Carbon steel is the default material for oil, gas, water and steam piping: adequate strength, good weldability and the lowest cost of the B16.5 material groups.
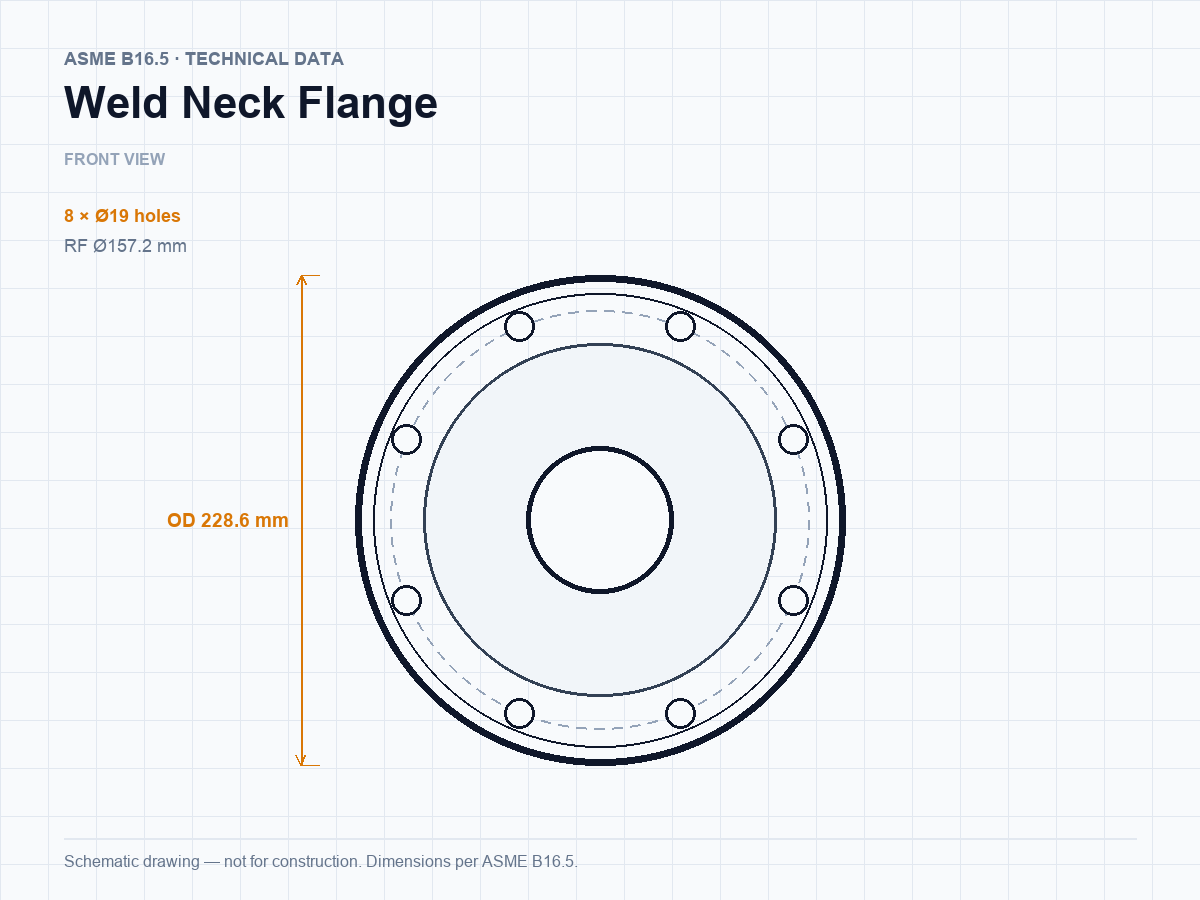
ASTM A105 is the standard forged carbon steel for flanges and fittings in ambient-to-moderate service. It is used across Class 150 to 2500 and is readily weldable, machinable and available in the full B16.5 size range. For low-temperature service down to −46 °C, A350 LF2 is the specified grade because it is impact-tested at low temperature. For higher yield strength in pipelines, A694 F52, F60, F65 and F70 are used with matching pipe grades.
Carbon steel flanges are normally supplied with a black oxide or anti-rust oil finish. Galvanising, epoxy or zinc-rich paint can be applied for atmospheric or buried service. We stock A105 in the common sizes and machine A350 LF2 and A694 grades to order, with MTC 3.1, heat-number marking and PMI verification on request.
Grades we machine and forge
| Grade | Specification | Service temperature | Typical use |
|---|---|---|---|
| ASTM A105 | ASME B16.5 Group 1.1 | −29 to 425 °C | General piping, steam, water, oil and gas |
| ASTM A105N | Normalised A105 | −29 to 425 °C | Improved toughness for low-temperature or impact-tested duty |
| ASTM A350 LF2 | Low-temperature carbon steel | −46 to 345 °C | Cold-service piping, LNG and refrigeration |
| ASTM A694 F52 | High-yield pipeline flange | −29 to 400 °C | Transmission pipelines, high-pressure gas |
| ASTM A694 F60 | High-yield pipeline flange | −29 to 400 °C | High-strength line pipe connections |
| Q235B / 20# | GB/T 9112–9124 | −20 to 350 °C | Domestic and general industrial piping |
Selection notes
- A105 is not recommended for wet sour service without hardness control and NACE MR0175 compliance.
- For service below −29 °C specify A350 LF2 with impact testing at the design temperature.
- Carbon steel flanges are supplied with anti-rust oil by default; painting or galvanising is available on request.
Welding and fabrication
- A105 welds readily with common carbon steel consumables; preheat is generally not required below 25 mm wall thickness, but thicker sections benefit from 100–150 °C preheat.
- Post-weld heat treatment is not mandatory for A105 in most services, but is specified where the joint is thick, restrained or exposed to sour service.
- A350 LF2 should be welded with low-hydrogen consumables and a controlled heat input to preserve low-temperature toughness.
- Galvanising is common for atmospheric and buried service; machined faces are usually masked to keep the gasket surface clean.
How to order
- State the standard, size, class, face type and quantity per size.
- Specify the material certificate: 3.1 as standard, 3.2 when third-party witnessing is required.
- For low-temperature or sour service, state the design temperature and the NACE requirement on the order.
- Confirm the coating: anti-rust oil, paint, galvanising or none.
Common specification mistakes
- Ordering a grade without stating the certificate level — 3.1 is the baseline, not an upgrade.
- Using 304/316 instead of the L grades on welded assemblies, then finding sensitisation at the weld.
- Treating a PN rating and an ASME class as interchangeable; the pressure may match and the bolt pattern will not.
- Specifying a material for sour service without checking the NACE hardness limit and heat-treatment condition.